The Ultimate Guide to Industrial Colour Label Printers
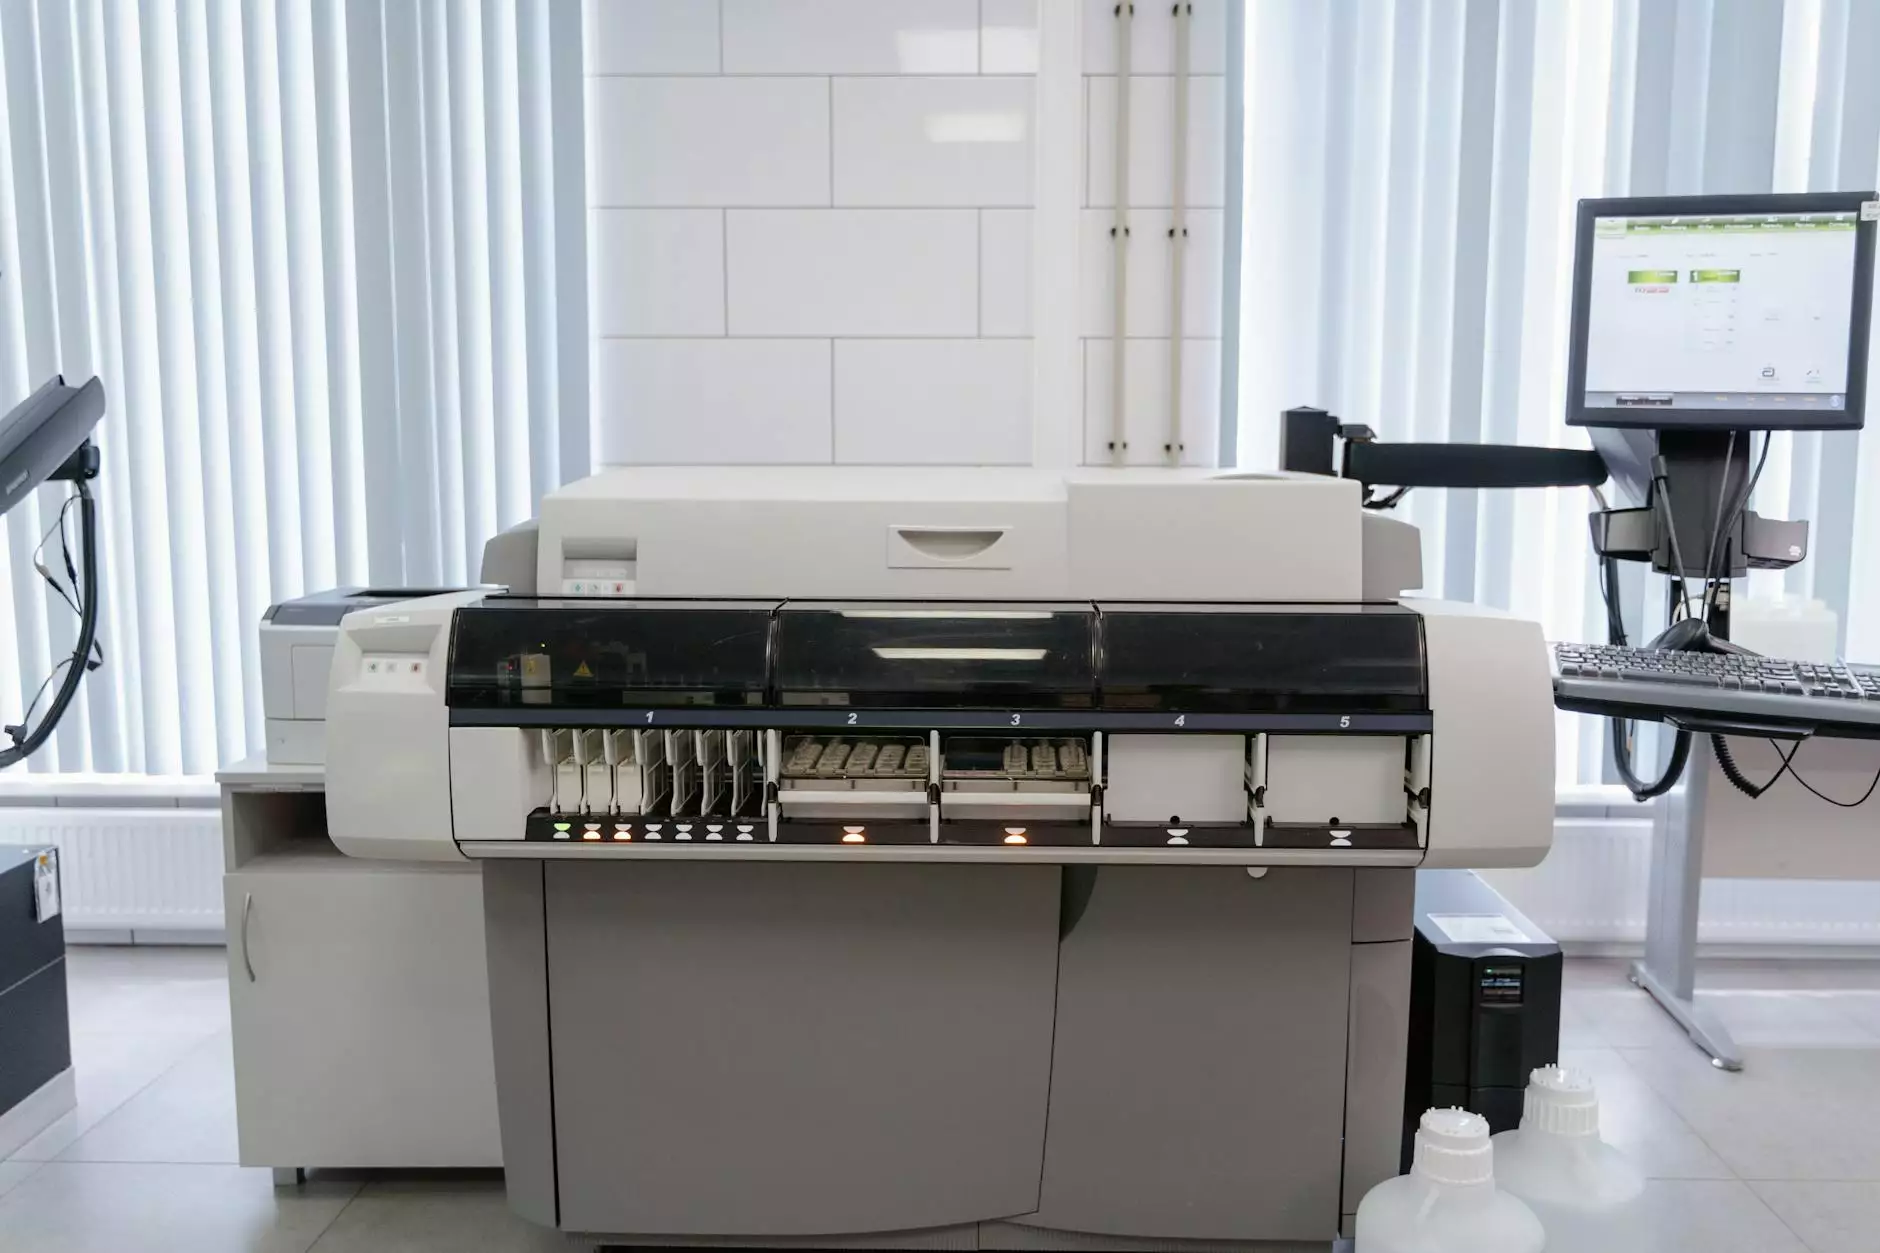
Industrial colour label printers have revolutionized the way businesses manage labeling needs, offering superior quality, efficiency, and flexibility. In an era where branding and compliance are paramount, understanding the significance of industrial colour label printers can empower your business to effectively meet its operational demands while elevating its market presence.
What is an Industrial Colour Label Printer?
An industrial colour label printer is a specialized printing device designed for producing high-quality labels in bulk. These printers are engineered to handle a variety of materials and offer exceptional printing speeds, making them ideal for industries that require robust labeling solutions. Unlike standard printers, industrial label printers are built for heavy-duty use, ensuring durability, efficiency, and cost-effectiveness.
Key Features of Industrial Colour Label Printers
- High Print Quality: Industrial colour label printers can produce vibrant, sharp images and text, essential for effective branding.
- Durability: These printers are built with robust components to withstand the rigours of continuous use in demanding environments.
- Speed: Capable of printing hundreds to thousands of labels per hour, they help streamline production processes.
- Versatile Media Handling: They can print on various label materials, including paper, vinyl, and synthetic substrates.
- Advanced Connectivity Options: Many models offer Wi-Fi, Ethernet, and USB connectivity for seamless integration into existing systems.
Applications of Industrial Colour Label Printers
The applications of industrial colour label printers are vast and varied, making them invaluable across multiple sectors. Here are some industries and their specific uses:
1. Manufacturing
In manufacturing, these printers are used for product labeling, compliance labels, and barcodes. They ensure that all products are accurately labeled, which is critical for inventory management and regulatory compliance.
2. Food and Beverage
The food industry requires strict adherence to labeling laws, including ingredient lists and expiration dates. Industrial colour label printers can print waterproof, smudge-proof labels that maintain quality and legibility under various conditions.
3. Pharmaceuticals
In the pharmaceutical industry, labels must convey critical information accurately. Industrial printers ensure that medication labeling complies with stringent regulations and maintains clear visibility for consumers.
4. Retail
Retail businesses use colour labels for pricing, promotions, and branding. Custom-printed labels can attract customers and support organized inventory management.
5. Logistics and Shipping
These printers are essential for creating shipping labels, barcodes, and tracking labels that support the efficient flow of goods through the supply chain.
Benefits of Using Industrial Colour Label Printers
Investing in an industrial colour label printer presents numerous advantages for businesses looking to enhance their labeling processes. Here are some key benefits:
Cost-Efficiency
While the upfront cost of an industrial label printer may be significant, the long-term savings are substantial. By producing labels in-house, companies can save on outsourcing costs and improve their profit margins.
Customization
The ability to create custom labels allows businesses to differentiate their products in a competitive marketplace. Whether you need specific branding elements or unique sizes, industrial printers offer flexibility and creativity in label design.
Reduced Lead Times
With the capability to print labels on-demand, businesses can significantly cut down on lead times associated with procurement processes. This flexibility allows for rapid response to changing market conditions and immediate adjustments to inventory branding.
Improved Inventory Management
Accurate and readable labels facilitate better inventory control. Industrial colour label printers help in generating barcodes that streamline stocktaking and scan efficiently, reducing human error in inventory management.
Choosing the Right Industrial Colour Label Printer
Selecting the right industrial colour label printer can feel overwhelming given the variety of options available. Here are critical factors to consider when making your choice:
1. Printing Technology
Different printers utilize various technologies, including thermal transfer, direct thermal, and inkjet. Each technology has its strengths, and understanding your needs will help in making the right decision.
2. Print Resolution
High-resolution printers produce clearer images and text. If your labels need to convey intricate designs or small text, opt for printers with higher DPI (dots per inch).
3. Printing Speed
Consider your production requirements when assessing printing speed. Some models can print over 300mm per second, which might be necessary for high-output environments.
4. Label Size and Material Compatibility
Ensure the printer can handle the size and material of labels that your business requires. Some printers are specialized for certain materials that may not be compatible with others.
5. Software and Integration
Check if the printer is compatible with your existing design and inventory management software. A seamless integration can enhance productivity and reduce training time.